أجزاء بلاستيكية لقفص الهامستر مخصصة

أجزاء بلاستيكية لقفص الهامستر مخصصة

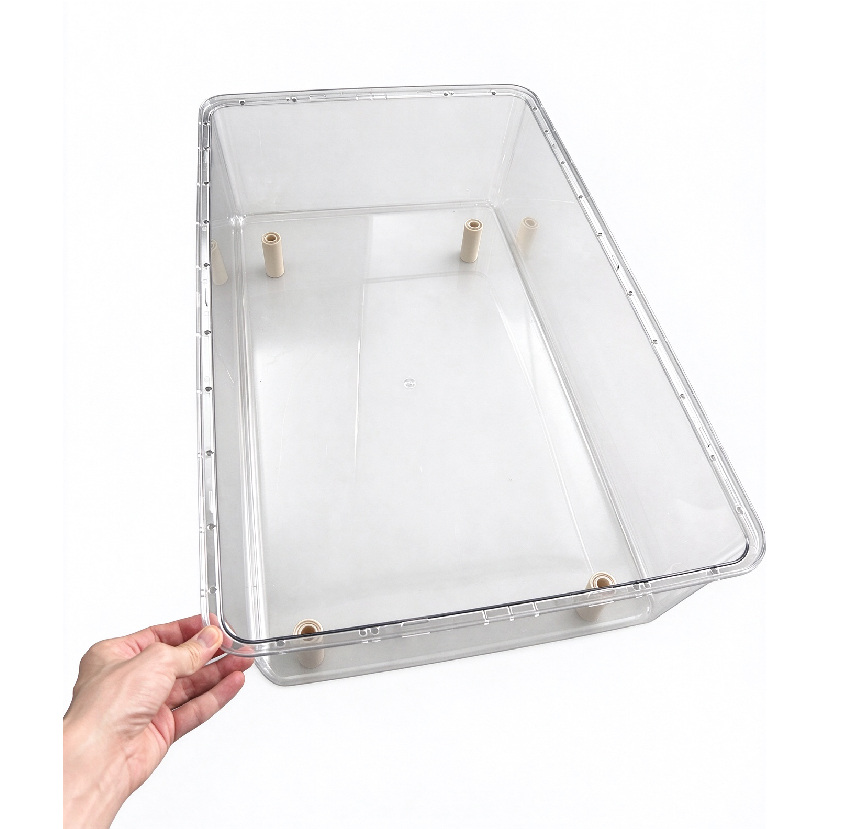
Custom fully transparent hamster house with OEM & ODM service. Clear plastic design for easy observation, custom size, structure, silk printing and stacking structure available.

  • We offer OEM / ODM injection molding service for custom plastic accessories of extra-large hamster cages. Whether you need pull-out waste trays, tunnel connectors, transparent shelters, base frames or other custom parts, we optimize the structure for assembly fit, stacking stability and easy cleaning.
  • All parts can be customized in material, color and surface finish. We provide DFM analysis, sample verification and mass production.

Extra Large Hamster Cage | Custom Plastic Accessories | Injection Molding | OEM ODM

1、Custom fully transparent plastic pet houses, play toys and reptile breeding enclosures. Premium clear material delivers excellent visibility for viewing your pets, 2、We support structural optimization, stacking design, custom color and surface finish, with DFM analysis and pre-production sample confirmation before mass production.

10000+
Monthly production capacity
35+
Countries Shipped
200+
Happy Clients
100%
Quality Guarantee

Inspection Specification for Product Structure and Mold Material

What the part is made of, which standards it is checked against, and on which equipment:

Part, Resin & Mold Industry Standards Core Inspection & Equipment
body - PET, virgin, fully transparent ISO 9001:2015 Material Specification
Mold cavity and core - S136 ISO 14001 CNC machining and EDM
Cavity surface - mirror polish, RoHS polish comparator plaques
Rim and lip - plain, no undercut Technical Specification CMM dimensional report per lot
Wall - 0.10 in nominal ASTM D256 impact Izod impact tester
Cooling - chilled mold, water circuits Mold Design Drawings Mold Temperature and Cooling System
Gating - large gate, low shear Mold Design Drawings First Article Inspection (FAI)

سيناريوهات الأعمال B2B وقيمة البيع بالجملة

How cage brands, pet chains, distributors and assembly plants buy a clear molded tub

Modular and Stackable Cage Systems

1. The basin supports the frame, instead of the frame supporting the basin. This allows a second layer to be stacked on top of the first layer to save space.
2. Corner posts are defined at the DFM (Design for Manufacturability) stage. This means only cavity inserts need to be replaced to adjust the layer height, rather than the entire mold frame. Both core and cavity inserts require modification.
3. The wall and bottom thickness are sized for strength based on weight analysis. The stacked main body will not deform under the load from the weight above.
Retail Display and Pet Chain Programs

1. Fully transparent pet enclosure: Live animals inside are visible to customers directly from the aisle, without the need for staff to open any cover.
2. The transparent hamster cage supports interior DIY setup and habitat decoration to simulate the natural living environment of small pets, facilitating observation.
3. The same mold is available for tinted clear, frosted and printed variants. For private-label products, differentiation can be achieved only by color adjustment.

Replacement Tub Programs

1. The tub is the part that cracks, scratches or discolours first, and it is the cheapest part of the cage to reorder.
2. We mold to the cage you already sell, so the replacement drops onto the existing posts with no change to the frame.
3. Tubs nest for shipping, so a pallet of replacements holds several times the volume of assembled cages.

Contract Molding for Cage Assemblers

1. We supply the tub to the assembly line on a scheduled call-off, not only as a finished retail pack.
2. Insert pull-out and dimensional reports travel with each lot, so the frame still bolts down after a tool service.
3. Tooling paid for by you is booked under your name and can be moved out on written request.

A clear tub that is also the base of the cage

A clear tub that is also the base of the cage

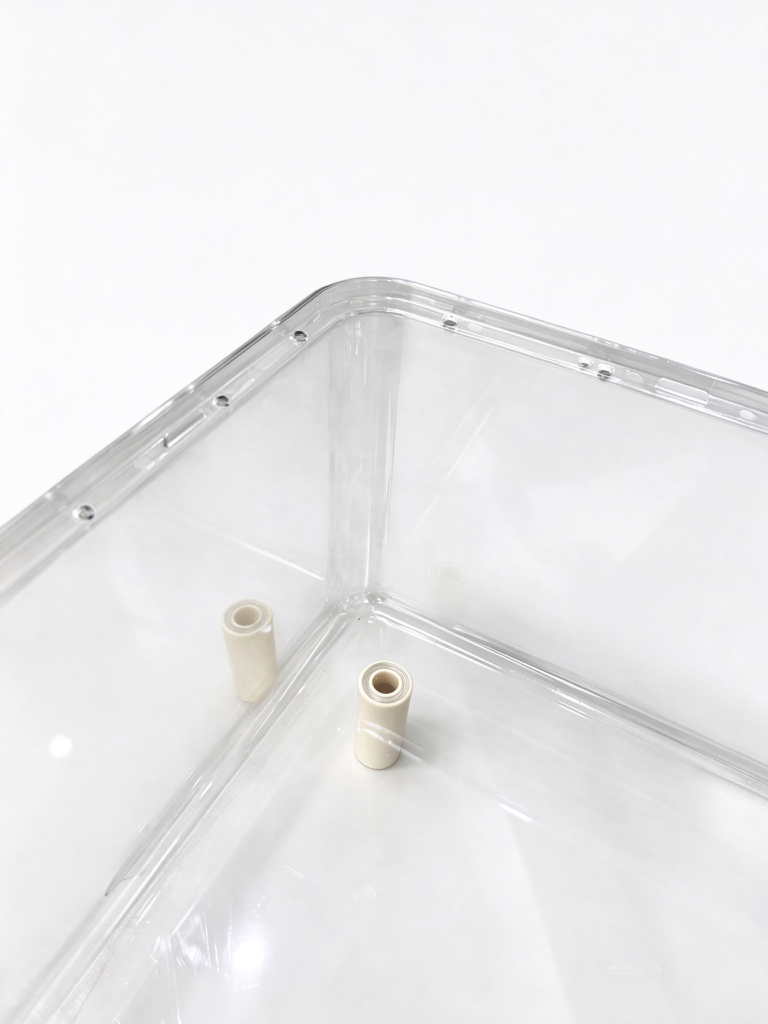
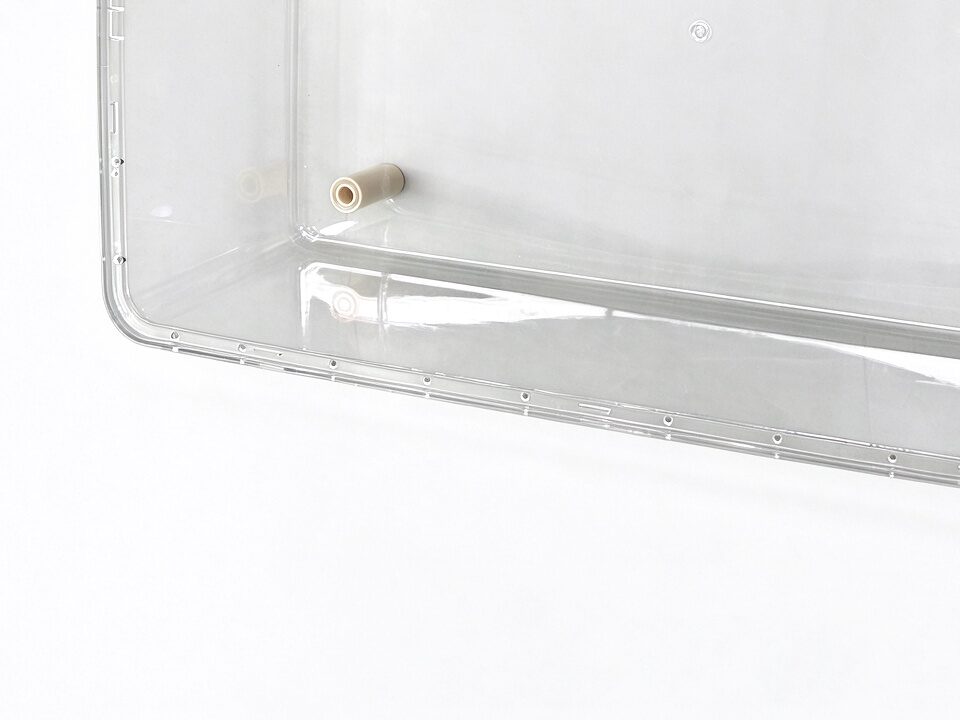
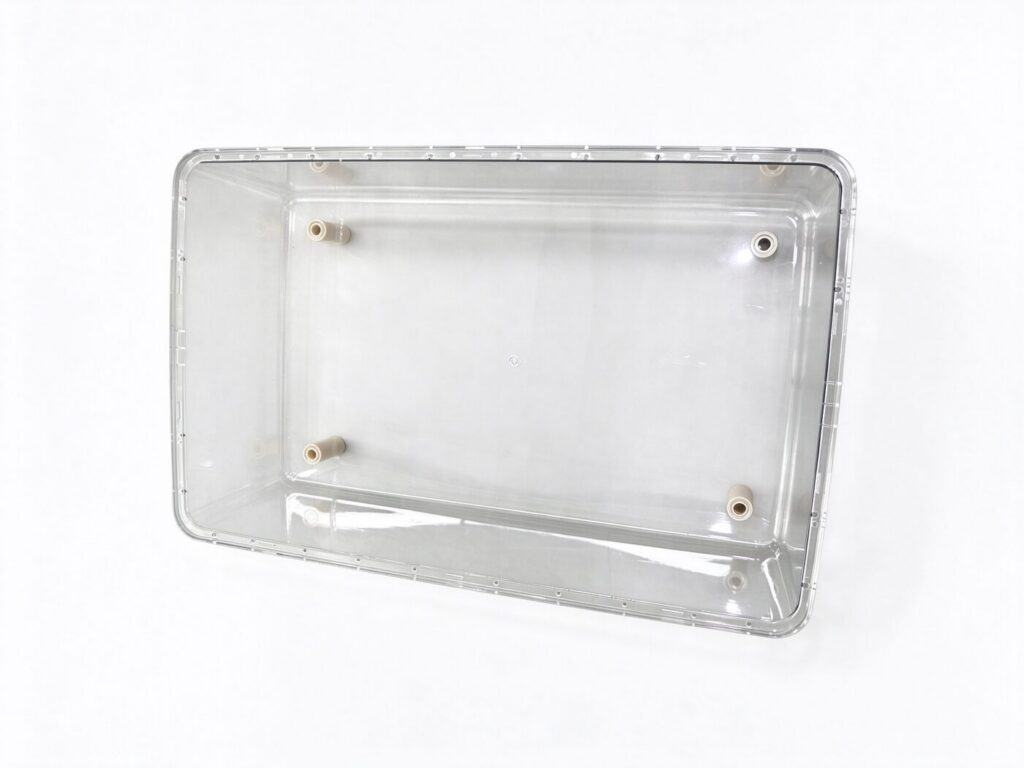
The corner posts on the four corners are used to support and secure the upper cage body, keeping the main housing off the ground. This makes the basin an integral structural part of the cage frame.
Large draft angles are applied on the upper and lower shells, which enables this stacking / modular system. The second-tier frame rests on the base main body; loads transfer down through the basin instead of being carried by the side walls.
There are no undercuts on the outer surface of the product. External latches are used instead. Therefore, this part can be demolded in a single-cavity mold without slide mechanisms.

Design Considerations for Hamster Cage Bottom Housing

Design Considerations for Hamster Cage Bottom Housing

1. The overall wall thickness shall be kept uniform to optimize plastic melt flow and cooling, and avoid wall thickness marks.
2. All corner sections adopt large fillet design, ensuring smooth material flow and convenient cleaning.
3. Draft angles comply with mold flow analysis. The design enables the top shell to nest within the bottom shell, minimizing packaging space.

Gate Location Selection for Hamster Cage Bottom Housing

Gate Location Selection for Hamster Cage Bottom Housing

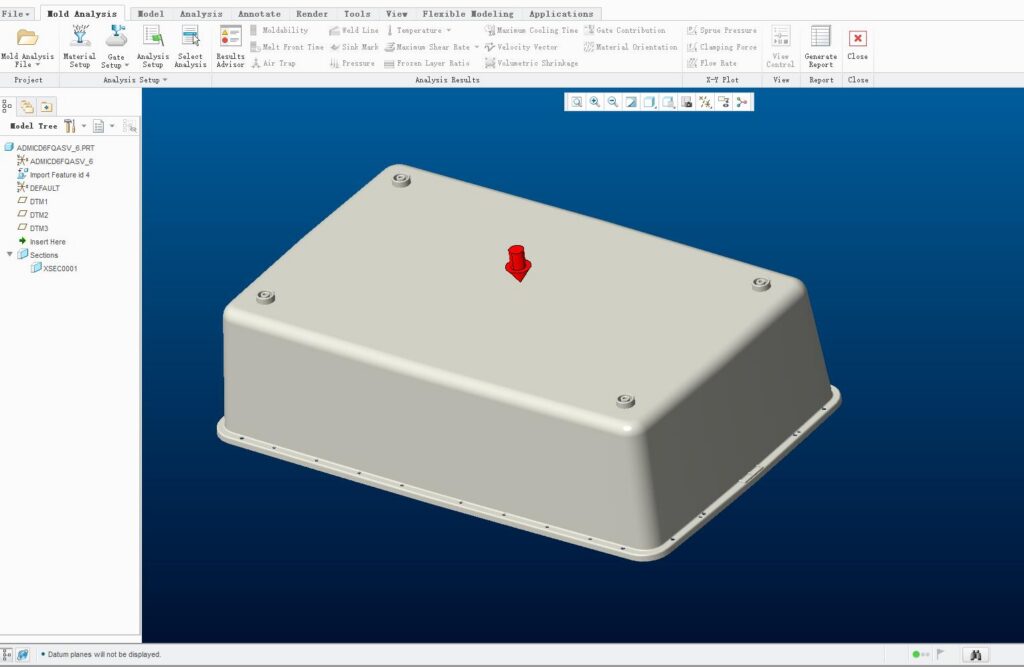
Our bottom shell adopts a sprue gate injection method that balances molding quality and cost control:

1. Fast filling, efficient shaping
The sprue gate rapidly fills the entire cavity and completes shaping with a short packing cycle, ensuring stable, efficient molding.
2. Single gate, no weld lines
Single-point gating prevents plastic weld lines formed by converging melt fronts, delivering a smoother surface and more reliable structure.
3. Simple mold, lower cost
The sprue gate allows a simpler mold structure, reducing tooling cost and directly lowering unit cost for better price competitiveness.

Clear, and it stays clear: the cavity decides

Clear, and it stays clear: the cavity decides

Transparency is a mold decision before it is a resin decision. An S136 cavity polished to SPI A-1 transfers no tool marks into the wall, and a chilled mold stops the PET from crystallising into white patches as it fills.
Resin is dried before every run, because moisture in PET hydrolyses in the barrel and leaves splay streaks that no amount of polishing removes afterwards.
That is the whole difference between a tub that reads as glass and one that reads as cloudy plastic.

This fully transparent bottom shell suits multiple scenarios

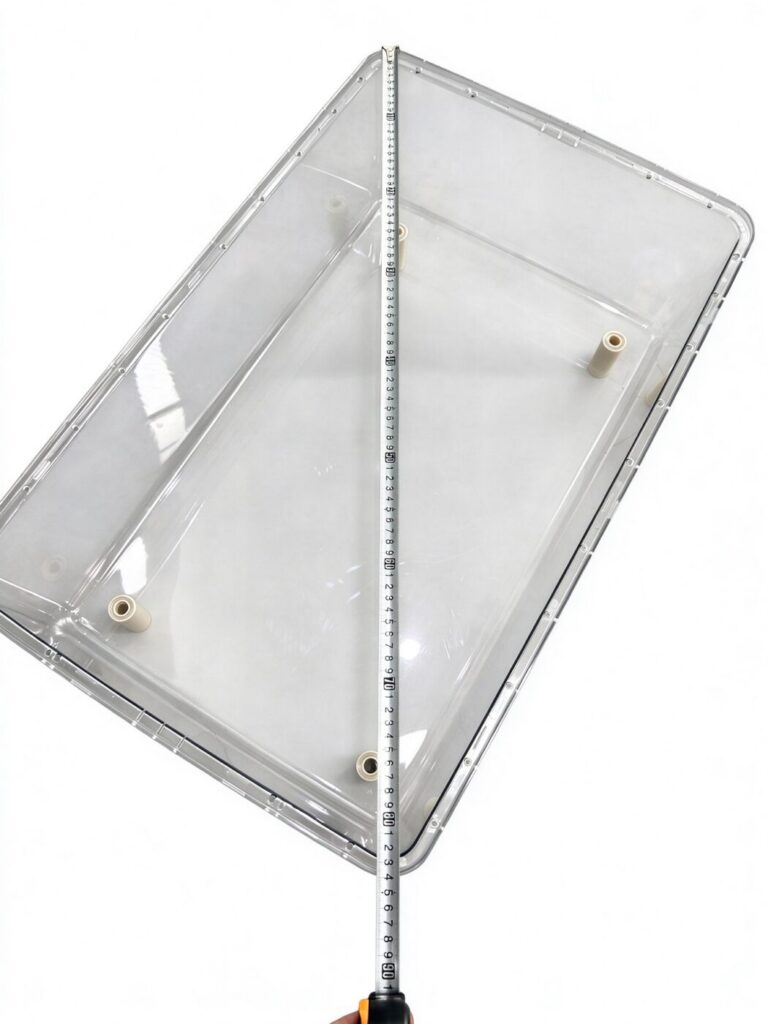
The same 29.5 x 18.5 x 8.1This fully transparent bottom shell fits a wide range of raising scenarios. It works perfectly for reptiles including turtles, chameleons, lizards and pet snakes. It is also suitable for small animals such as button quails.

Hamster and Small Animal Cages

A deep clear base gives a hamster room to burrow while the owner can still see it. The 8.1 in depth is what makes a proper bedding layer possible without a lid that hides everything.

Fully Transparent Bottom Shell for Lizard Keeping

This roomy, fully transparent bottom shell offers ample interior space. You may arrange wooden climbing ornaments to create a natural habitat for lizards. The clear design lets you easily view your pet’s activities and observe their feeding and exploring behaviors up close.

Retail Display and Education

This enclosure is suitable for animal display in shops and classrooms.
First, when used in classrooms or research institutes, it supports teaching activities. Learners get a close view of animal movements and living habits, which helps them build a better understanding of small animals.
Second, for retail store displays, realistic living scenes can be arranged inside the transparent bottom shell, with tailored setups to suit different species.

Modular pet enclosure for small pets and reptiles, easy to stack and expand.

Perfect for pet merchants who raise multiple species. Featuring stackable and expandable construction, this enclosure can be stacked into 3–5 tiers to greatly save storage and display space. You can place larger, heavier animals on the bottom level, while lighter pets are housed on the upper layers in sequence.

Design Notes for a Transparent Hamster Cage Tub

To produce crystal-clear plastic parts instead of hazy ones, four key factors matter: mold steel, polishing process, material selection, gate design and cooling system.

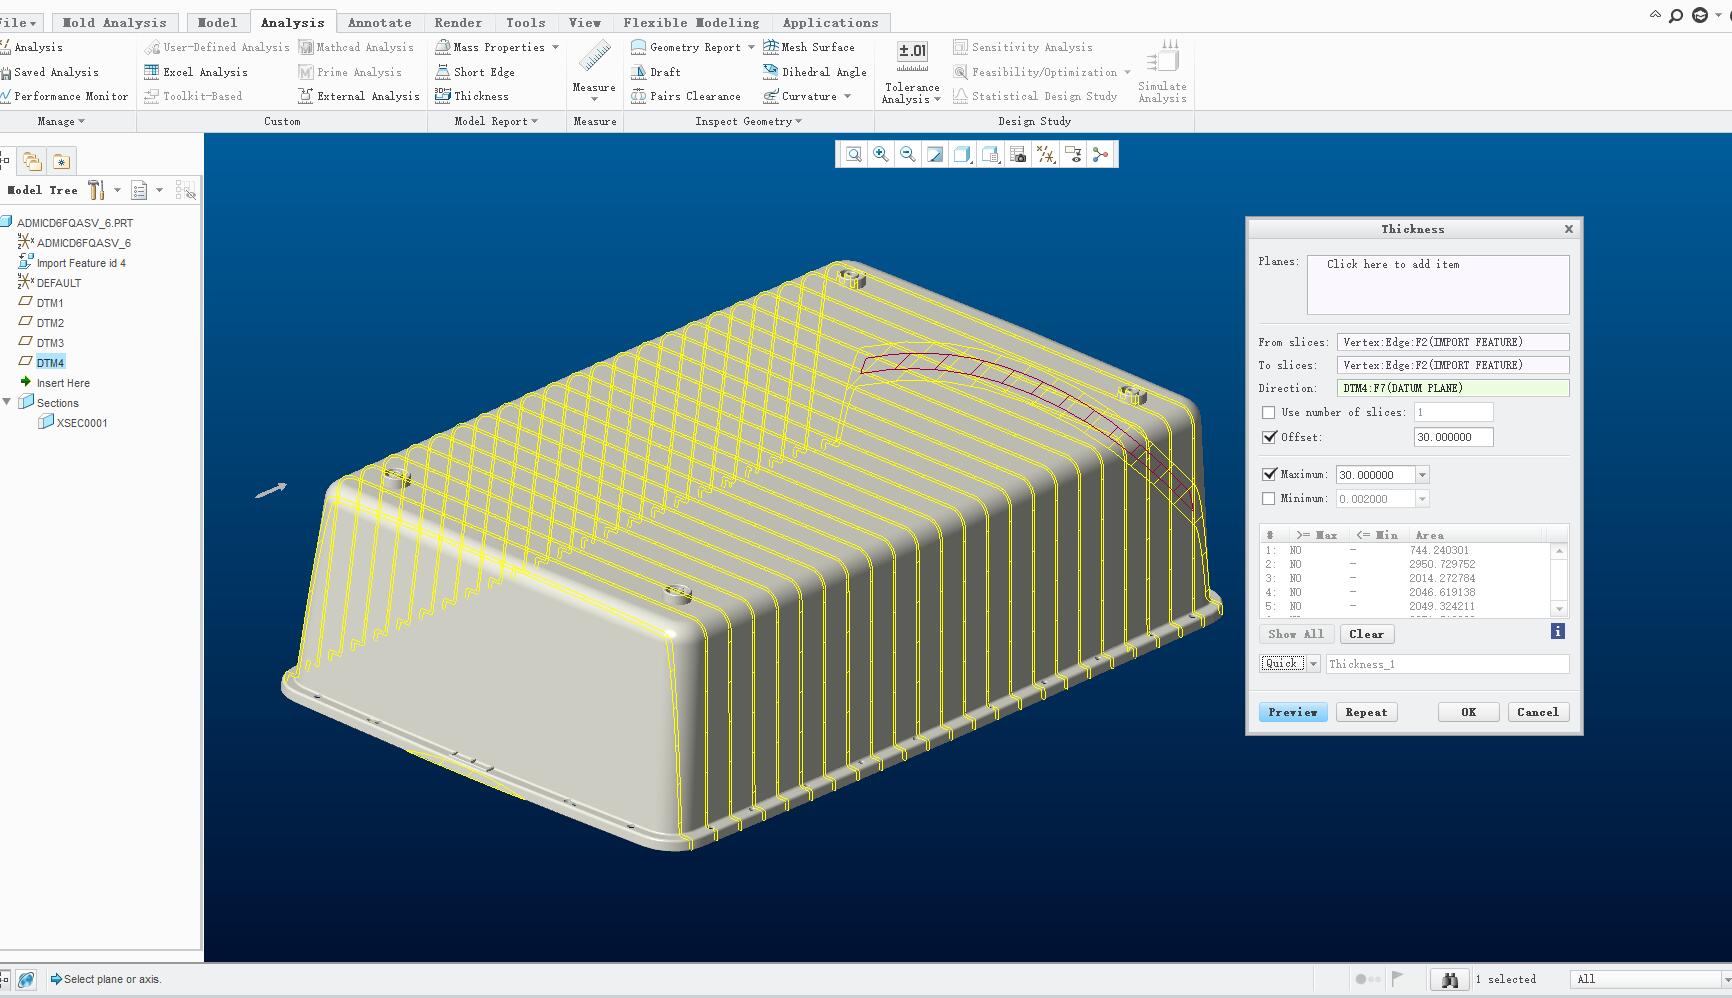
Thickness Analysis Statement for Fully Transparent Bottom Shell

Thickness Analysis Statement for Fully Transparent Bottom Shell

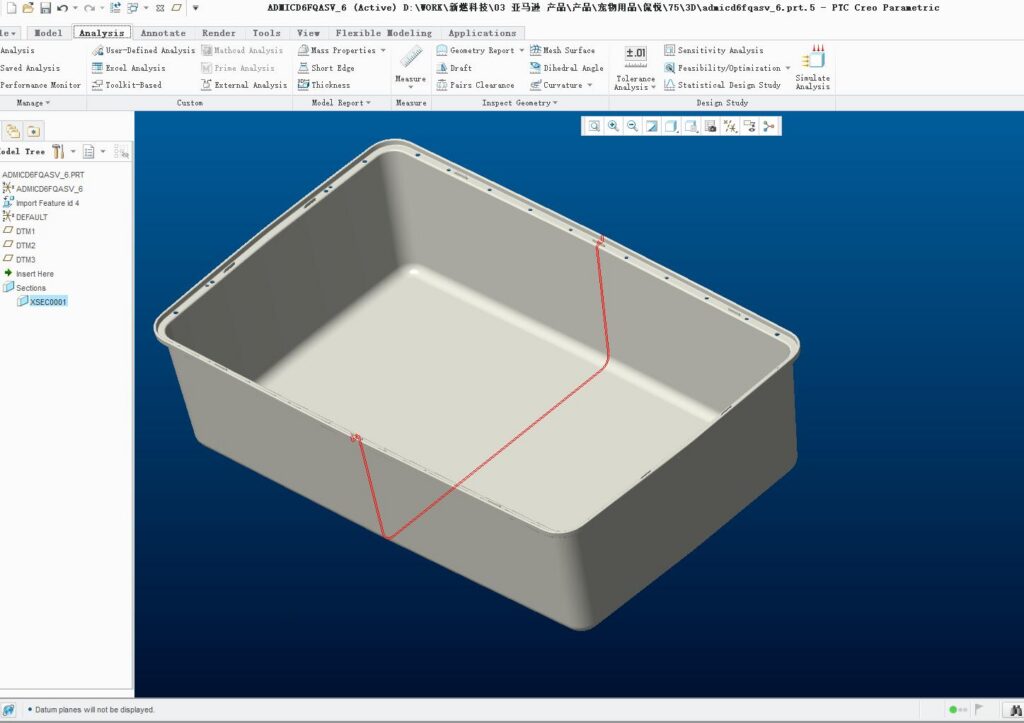
We carry out cross-section analysis of the model in 3D CAD software to configure smooth transitions between the minimum and maximum wall thickness values. Where the simulation detects improper thickness ratios, our engineering team adjusts the design to guarantee gradual transitions. With parametric design, we precisely achieve the ideal performance targets required by the customer.

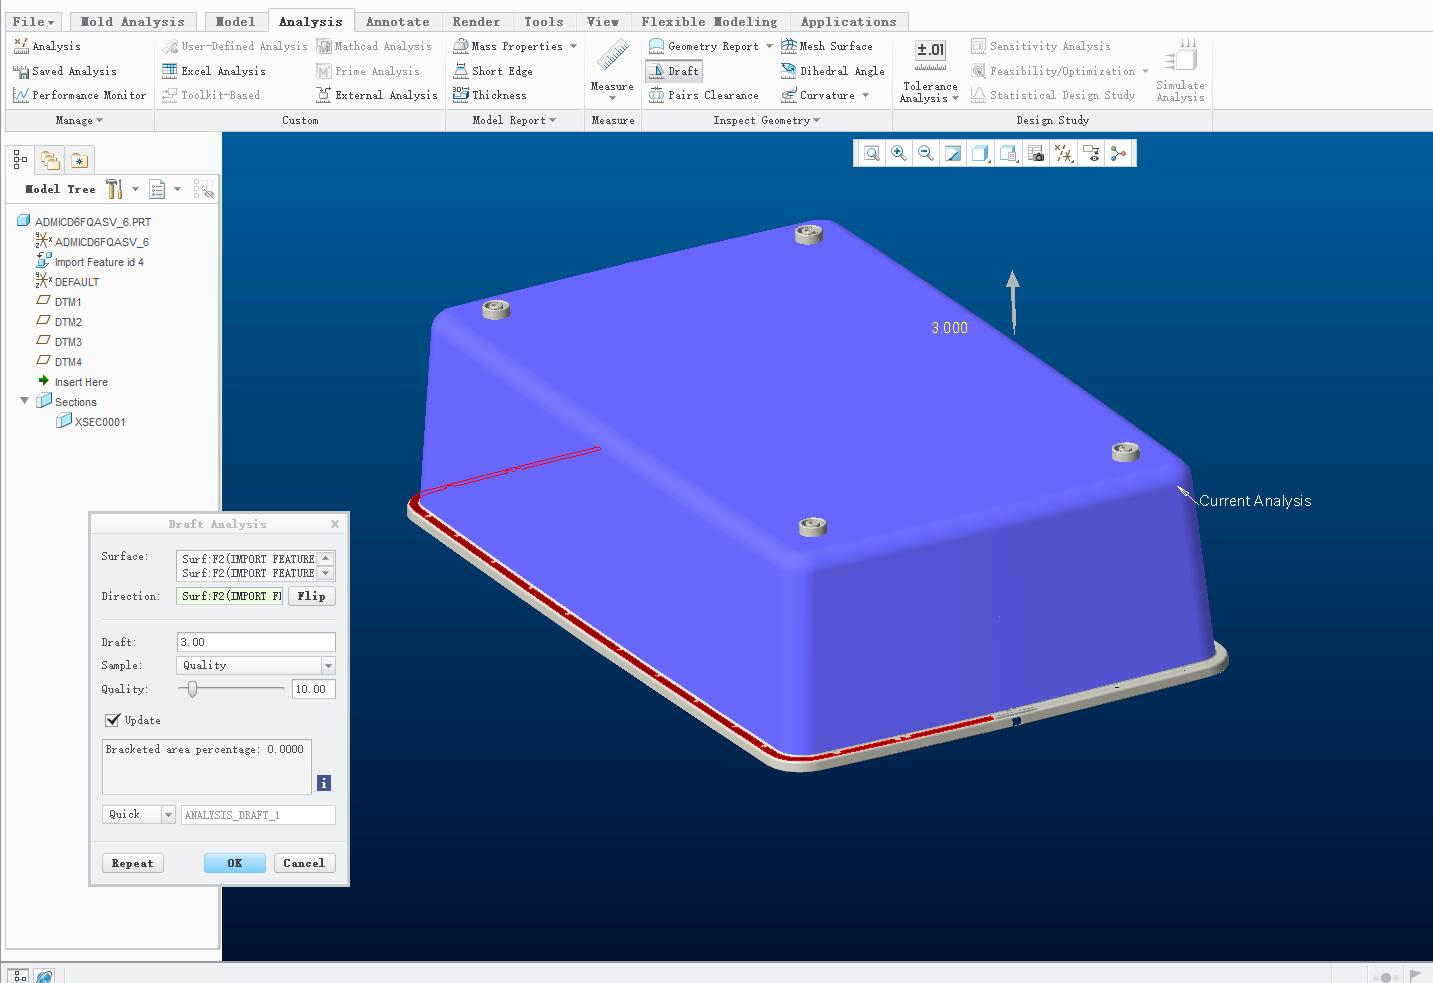
Angle Analysis of Plastic Parts Prior to Mold Manufacturing

Angle Analysis of Plastic Parts Prior to Mold Manufacturing

The plastic component is imported into 3D software to finalize mold manufacturing parameters, including mold process plan, parting direction and injection gate configuration. We analyze ejection draft angles carefully to ensure all features on every surface are provided with adequate draft. This avoids scuffing on the part during demolding and eliminates related appearance defects.

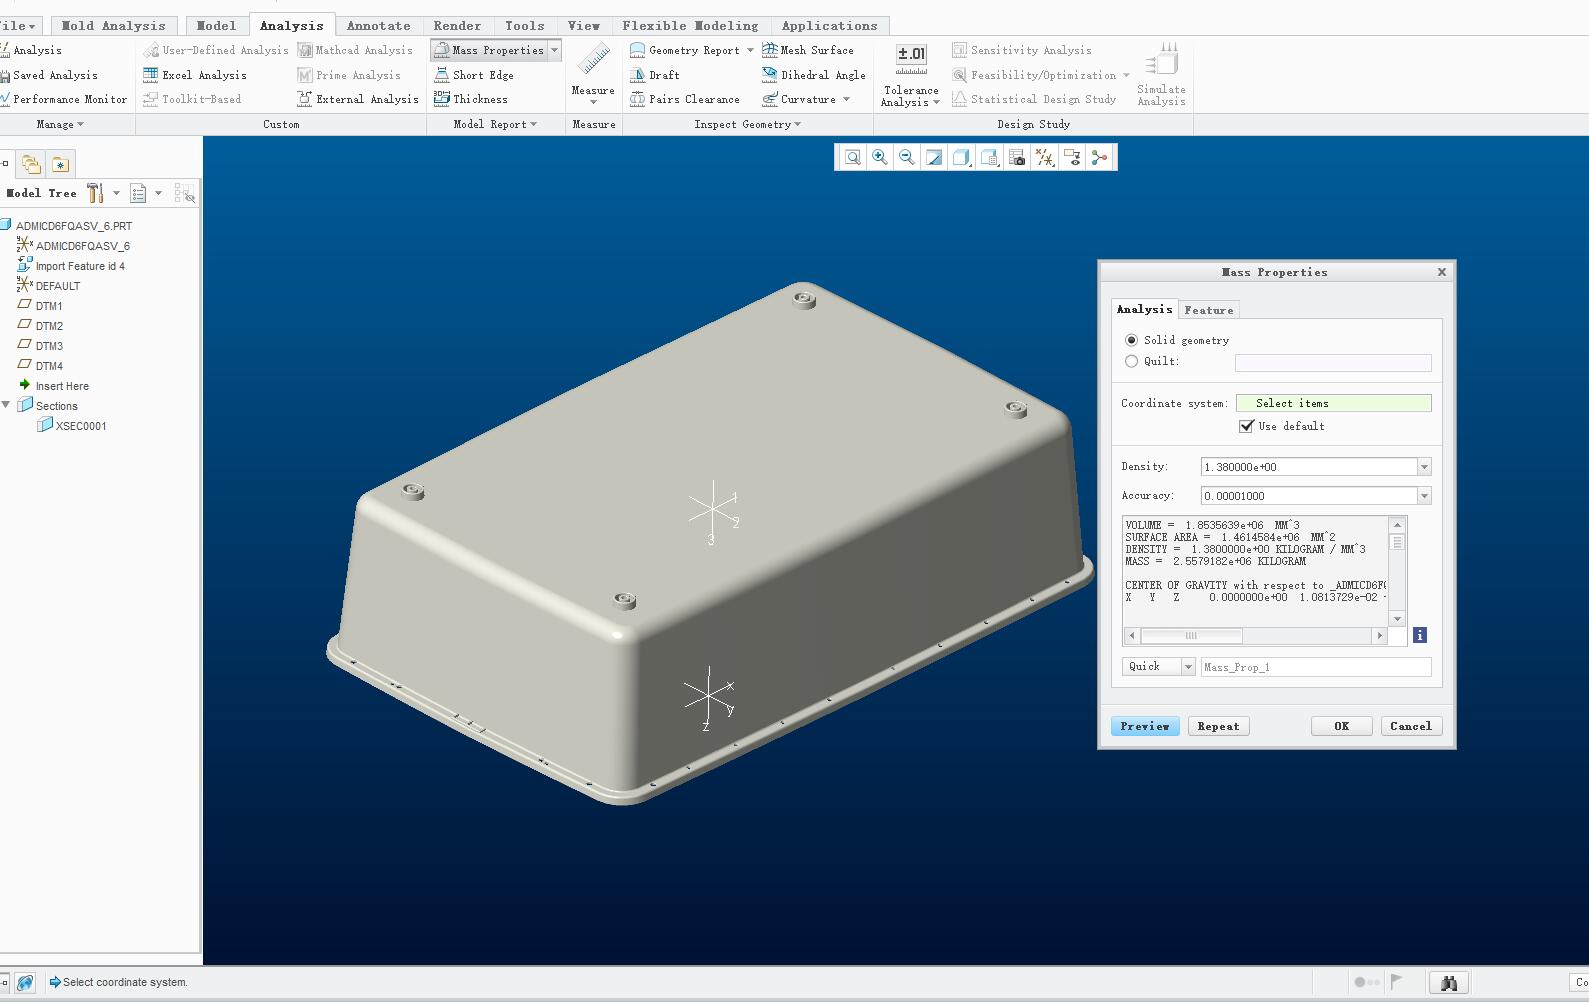
Simulate and calculate the material weight of the component to accurately estimate the unit cost.

Simulate and calculate the material weight of the component to accurately estimate the unit cost.

Once the transparent raw material is confirmed, parameter analysis covering product weight and center of gravity will be performed. With accurate material density input, we can compute the actual weight, structural strength and other key indicators. This extra verification helps ensure the finished part complies with all requirements.

Drying and chilling decide the clarity

Drying and chilling decide the clarity

Moisture in the pellets becomes splay streaks; a warm cavity becomes white crystallised patches. The resin is dried before every run and the mold runs chilled, so the wall stays clear where it touched the steel.

Commercial Terms & Certification

الحد الأدنى للطلب OEM/ODM

Custom tint, logo and retail packaging start at 500 pcs.

Samples are available from a single unit, machined or from a T1 shot.

مهلة الإنتاج

Tooling and T1 samples (S136, mirror polish) 15-20 working days after DFM sign-off

Pilot run and approval 5-7 working days

Mass production, 500 pcs 12-18 working days

Sea freight to EU or US 35-45 days

التغليف القياسي

1pc x Clear PET tub

1pc x PE bag, rim protected

10pcs x Export carton, tubs nested

Tubs nest, so a pallet holds several times the volume of assembled cages

Custom retail carton quoted separately

Prices are quoted against a confirmed drawing, resin grade and quantity. Tooling is charged once and stays in production for repeat orders.

Certification Support

We prepare the material and test documents for the certifications below and run pre-shipment checks against them, so your own compliance file is complete before the container leaves.

RoHS REACH SVHC ISO 9001 PAHs

Looking for Customization or Bulk Orders?

From a single sample tub to a container of nested tubs - tooling, molding, inserts, packing under one roof.

How to Choose Clear Raw Material for Transparent Molding

Available transparent engineering resins cover PMMA, PC, PET and PP. It is necessary to clarify the intended application, load requirements, light transmittance specs and surface requirements of the part.

PET material can be selected for applications requiring light transmittance above 90% and medium strength with a load capacity of 50 kg. It delivers excellent cost-performance ratio for cost reduction. PET material can be selected for applications requiring light transmittance above 90% and medium strength with a load capacity of 50 kg. It delivers excellent cost-performance ratio for cost reduction.
Large injection molding equipment is required for one-piece molding of this extra-large fully transparent shell. The molding process operates with high injection pressure and high clamping force. Large injection molding equipment is required for one-piece molding of this extra-large fully transparent shell. The molding process operates with high injection pressure and high clamping force.

Why PET, and why the mold decides the clarity

A transparent cage tub is bought for one reason: the animal stays visible. PET gives that clarity at a lower resin cost than polycarbonate, and it takes a tint without going milky. The trade-off is process discipline. PET absorbs moisture from the air, and any moisture left in the pellets turns into steam in the barrel, which shows up on the finished wall as silver streaks.

Clarity is then decided a second time in the tool. An amorphous resin has to be cooled fast, so the cavity runs chilled; if the mold is warm, the surface crystallises and turns white where it touched the steel. The cavity itself is polished, because every tool mark prints through a clear wall. That is why the specification here names S136 and SPI A-1 rather than just the resin.

Successful Case Introduction: Transparent Hamster Cage Tub

Case A - Clear PET base tub for a modular small animal cage
Part: one-piece clear tub with a plain rim and four corner posts carrying threaded inserts
Material: PET, virgin, fully transparent amorphous grade
Size: 29.5 x 18.5 x 8.1 in overall
Mold: S136 stainless, hardened to 52 HRC, cavity mirror polished to SPI A-1, chilled water circuits

What the project needed: the tub had to take the frame screws itself, so the four posts and their inserts were positioned from the cage drawing rather than from the tub. Draft was kept at 1.5 deg on the side walls to release an 8.1 in deep draw without dragging the polish, and a large low-shear gate was used so no flow mark sits on the front face.

Result: the tub ships as the base of a modular cage and as a replacement part, from the same cavity and the same resin batch.

Technical Specifications

الخامة

PET, virgin, fully transparent (amorphous grade)

الحجم الكلي

29.5 x 18.5 x 8.1 in

Process

Injection molding, single-cavity

Mold steel

S136 stainless, hardened to 52 HRC

Cavity finish

Mirror polish, SPI A-1 on the visible faces

Nominal wall

0.10 in

Draft angle

1.5 deg on the side walls

Corner posts

4 posts, threaded brass inserts molded in

Thread size

Matched to the screw you specify

Clarity

Clear, no visible splay or flow mark on the front face

الحد الأدنى للطلب

500 pcs for custom tint, logo and packaging

التغليف

1 pc per PE bag, 10 pcs per export carton, nested

From Cage Drawing to Molded Batch

الخطوة 1 Requirement and DFM - send the cage drawing, the frame screw positions, the bedding depth you need and the quantity. We return a DFM report with draft, wall, gate and insert positions before a tool is cut. Send Requirements
الخطوة 2 Mold Making and T1 Samples - S136 cavity cut and mirror polished, T1 shots in dried PET, clarity checked against a polish and haze reference plaque.
الخطوة 3 Pilot Run and Approval - 50 to 100 pcs on the released tool, insert pull-out checked, tub fitted to your frame before the batch is released.
الخطوة 4 Mass Production - 500 pcs and up on the released tool, cavity pressure and cooling time logged every cycle, wall thickness checked on the first shot of each shift.
الخطوة 5 Packing and Shipment - tubs nest, so a pallet holds several times the volume of assembled cages. Lot dimensional report, resin certificate and the RoHS / REACH file go in the carton.

الوثائق والموارد الفنية

Which PET grade do you mold, and why not polycarbonate?

Amorphous PET is the default for a clear tub: it has the clarity and the light weight at a lower resin cost, and it takes a tint cleanly. Polycarbonate is the answer when impact strength matters more than clarity or when the part has to take a snap fit. Tell us the end use and we name the grade in the quotation instead of leaving it open.

How do you stop the clear walls from going hazy?

Two different causes, two different fixes. Moisture in the resin hydrolyses in the barrel and leaves silver splay streaks, so the pellets are dried before every run. A warm cavity lets the surface crystallise into white patches, so the mold runs chilled. After that it is polish: any tool mark prints through a clear wall, which is why the cavity is finished to SPI A-1.

Why is the mold made of S136 instead of P20?

S136 is a stainless tool steel that hardens to about 52 HRC and takes a mirror polish to A-1. A clear part needs that polish, and PET releases traces of acetic acid that will corrode a plain steel cavity over time. The polish survives far longer in S136, which is what keeps tub number one and tub number one hundred thousand looking the same.

Can the corner posts and inserts be moved?

Yes - insert positions are part of the DFM stage. Send the frame drawing and we place the posts to your screw pattern. If the pattern changes later, the post area can be run as an interchangeable insert so the main cavity does not have to be re-cut.

Will the tub fit a cage frame we already make?

Send the frame drawing or a sample. The outside profile and the post positions stay as they are, and the changes are made inside: rim height, wall section and the clearance at the posts. That is usually cheaper than changing the frame around a new tub.

FREQUENTLY ASKED QUESTIONS - HAMSTER CAGE TUBS

What is the minimum order, and what does the first order include?

Custom tint, logo and retail packaging start at 500 pcs. The first order normally includes the tool, T1 samples, a pilot run of 50 to 100 pcs and the dimensional report. Samples before that stage come from a single unit.

How is the tub priced - by weight or per part?

The quoted price is per part, built from the shot weight in PET, the cycle time on the tool and the packing you ask for. We show the shot weight in the quotation so you can see what the resin contributes.

ما الملفات المطلوبة لعرض السعر؟

Please send a 2D drawing or a 3D file of the tub (STEP or IGES), the cage frame drawing with the screw positions, the tint reference, the order quantity and any testing requirements. For a new development, please share the product specification and function list.

Can you supply the top section or lid as well?

Yes. The upper section is a separate part on its own tool and can ship with the tub as a set or separately as a spare. If you already have a top, send its outline and we mold the rim to suit it.

كيف تحمون تصميمنا وقوالبنا؟

An NDA is signed before drawings change hands. Tooling paid for by you is booked under your name and can be moved out on written request; we do not quote the same custom profile to another buyer.

What is the lead time for a repeat order?

Repeat orders run 12-18 working days for 500 pcs once the tool is released and the resin is in stock, plus sea freight. If the tint needs a new master batch, add 5 working days for the match and the plaque.

لماذا تختارنا

Top Tier OEM/ODM 20+ Years | Custom Large Smart Pet Products

أكثر من مليون
Annual Capacity
30+
R&D Team
ODM/OEM
20+ Years
الشهادات
CE/FCC/RoHS/FDA/IEC62368

الشهادات الدولية

نحن شركة عالية التقنية تجمع البحث والتطوير والإنتاج والمبيعات، ولدينا فريق متخصص في التصميم الصناعي والإلكتروني والإنشائي. حاصلون على ISO9001 وBSCI ونخدم أكثر من 200 عميل حول العالم.

الشهادات الدولية
FCC
CE
CE-EMC
REACH
RoHS
UN38.3
IEC62368
FDA
FCM
GPSD
UL/ETL IEC62368-1
FCM EU 10/2011
UL94

اتصل بنا نحن

يسعدنا التواصل معك!

العودة إلى جميع الخدمات