حاوية بلاستيكية للزواحف مخصصة

حاوية بلاستيكية للزواحف مخصصة

We provide a one-stop design and manufacturing solution for reptile enclosures.

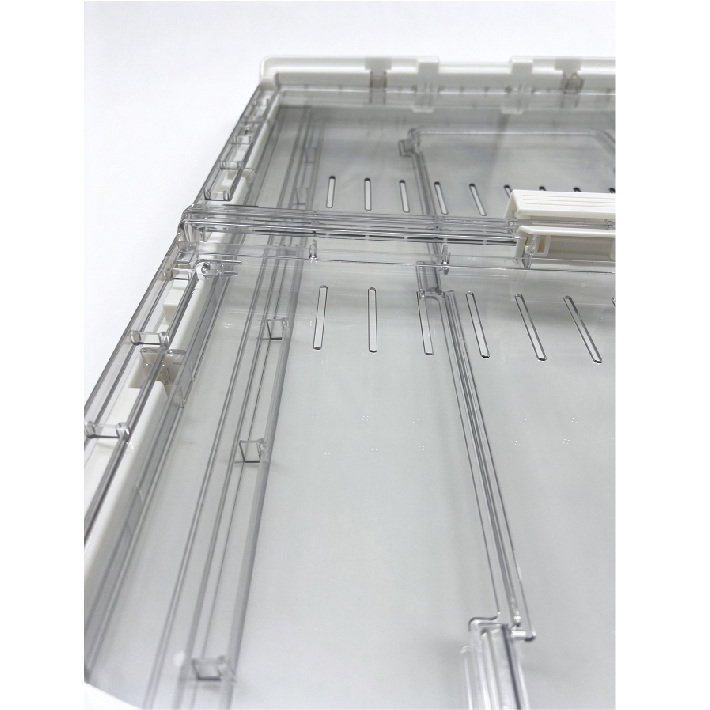
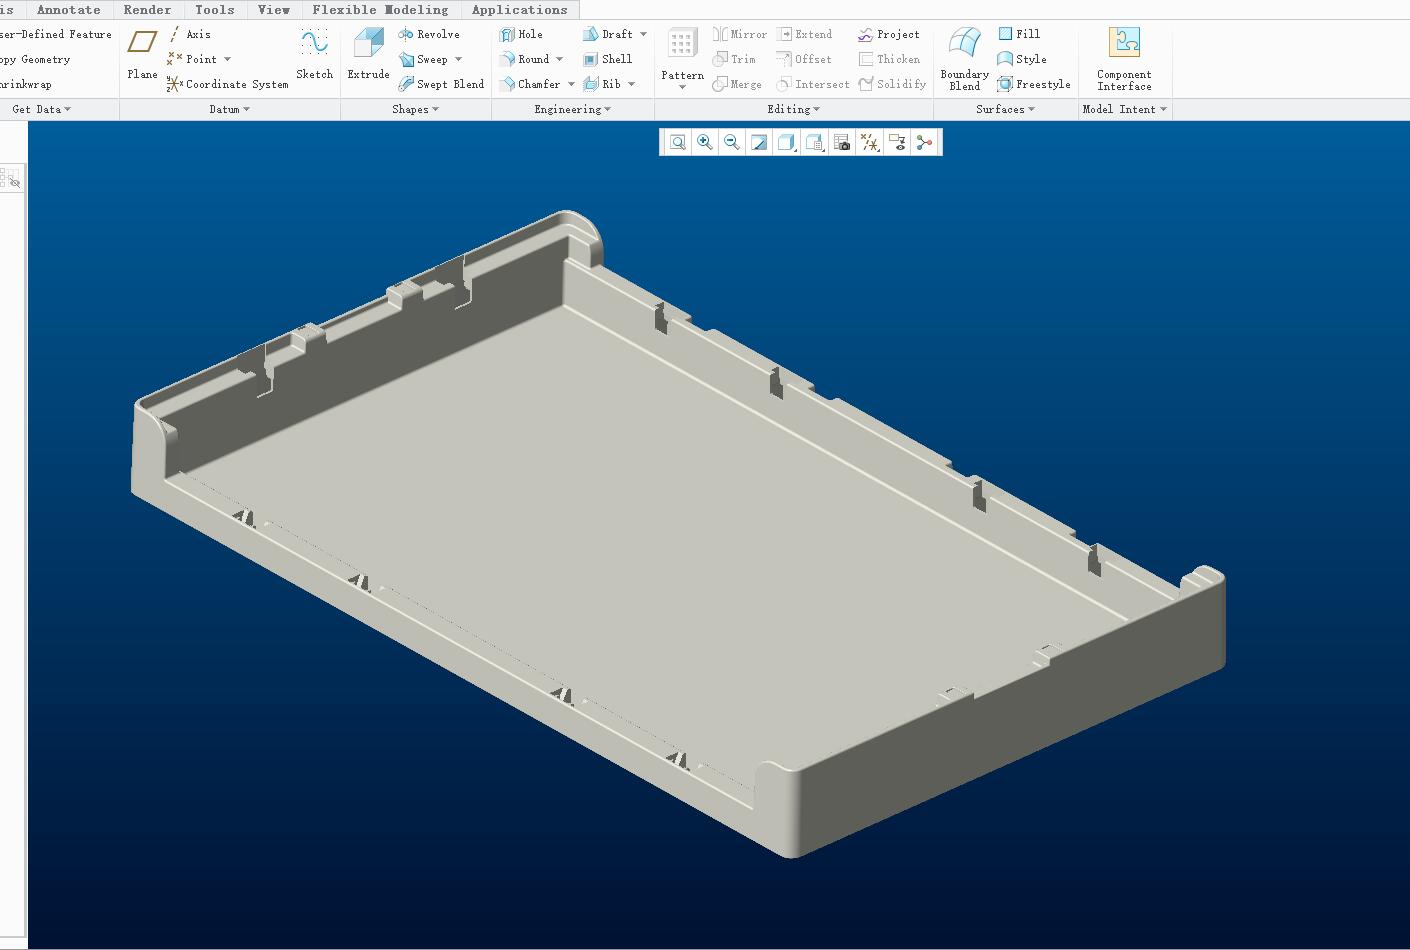
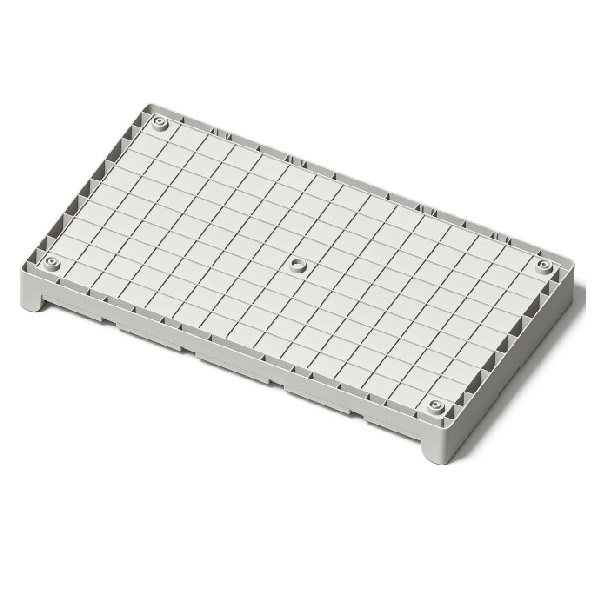
  • 1. This base is developed exclusively for folding pet enclosures. Since heavy decorations including simulated stones and driftwood are placed inside for reptiles, adequate structural rigidity is mandatory for the bottom housing. Reinforcement ribs are designed to support the whole base. Peripheral grooves enable the all-transparent side walls to fold inward for compact storage.
  • 2. After folding, the footprint is minimal. Compared with integrated one-piece pet habitats, it delivers substantial logistics savings.
  • 3. This folding enclosure is suitable for hamsters, quails, meerkats, sugar gliders, horned frogs, turtles, pet snakes and more.
  • 4. The base is integrally molded from high-strength food-grade ABS. It supports straightforward cleaning and can be washed directly under running water.

Custom Plastic Mold for Large Lizard & Sugar Glider Pet Enclosure Base

20,000+
Monthly Production Quantity
20+
Countries Shipped
100+
Happy Clients
100%
Quality Guarantee

OEM & ODM Service: Key Details for Large Reptile Plastic Products and Molds

Important Information List for Product Design and Plastic Tooling Design & Manufacturing

Plastic Product Information Plastic Tooling Information Inspection Standard Reference
Base Material: ABS Mold Steel Grade: 718H MTC / EN10204 3.1
Fence Material: PET Mold Steel Grade: S136 MTC / EN10204 3.1
ABS surface - matte texture Mold Cooling Circuit: Dual 3D Cooling Channels Texture plate or reference sample
PET surface - matte texture Gate Type: 1 large open gate reference sample
Base Wall Thickness: 0.1 in Injection Machine: 1500T Vernier Caliper/Tape Measure
Draft Angle: 1.5° Ejector Pins: Evenly distributed Angle Gauge
Reinforcing Ribs: Equally spaced array Part Ejection: Robot-assisted demolding Vernier Caliper
Rib Thickness: 0.045 in Mold Dimension:37.4 in Vernier Caliper/Tape Measure
Base Shrinkage Rate: 0.5% Side Actions: 12 sets of side cores Industry & Raw Material Standards
Base Warpage Control: 1‰ Flat Ejector Pins: 10 pcs Vernier Caliper/Height Gauge

سيناريوهات الأعمال B2B وقيمة البيع بالجملة

How enclosure brands, private labels, rack builders and breeding operations buy a clear tub and its base

Enclosure Brands Adding a Size

1. Product line expansion is normally achieved by introducing new outer dimensions rather than revising core structures. The top cover, locking latches and stacking interface remain consistent. Only the base requires new mold fabrication, while the surrounding side fences are reused to minimize tooling investment.
2. Uniform stacking height and latch mating positions are adopted across all sizes. Merchants can stock and use both outline variants mixed on the same shelf. Custom development of dividers and drawers is supported.
3. Ventilation layout, divider grooves and lid openings are built-in mold structures. Accordingly, no new assembly drawings are needed when adding new product variants.
Private Label and Retail Chains

1. Direct printing of brand markings on the fully transparent folding pet habitat undermines its key visual selling feature. For this reason, logo printing is arranged on the ABS base and outer packaging carton.
2. The base is colored via masterbatch dosing. A single mold cavity can produce parts in different colors, expanding the variety available for retail display.
3. We include retail color boxes, inner packaging bags and barcode labels within the quotation scope. The products are fully packaged and ready for retail placement once received by the customer.

Contract Molding for Terrarium Assemblers

1. We run the tub and the base as a scheduled call-off to your assembly line, not only as a finished retail box.
2. A dimensional report travels with every lot, so a base molded this month still takes a tub from a tool serviced last year.
3. Tooling paid for by you is booked under your name and can be moved out on written request.

Replacement Lids and Bases

1. The lid is the part that goes first - it is the part that gets opened, dropped and stood on edge.
2. Both clear parts and both ABS parts stay in the same tool family, so a replacement lid still seats on a tub molded two years earlier.
3. Spares ship nested and stack flat, which keeps a distributor's warehouse depth down.

Custom collapsible reptile enclosure with fully transparent PET panels and injection molded ABS base.

Custom collapsible reptile enclosure with fully transparent PET panels and injection molded ABS base.

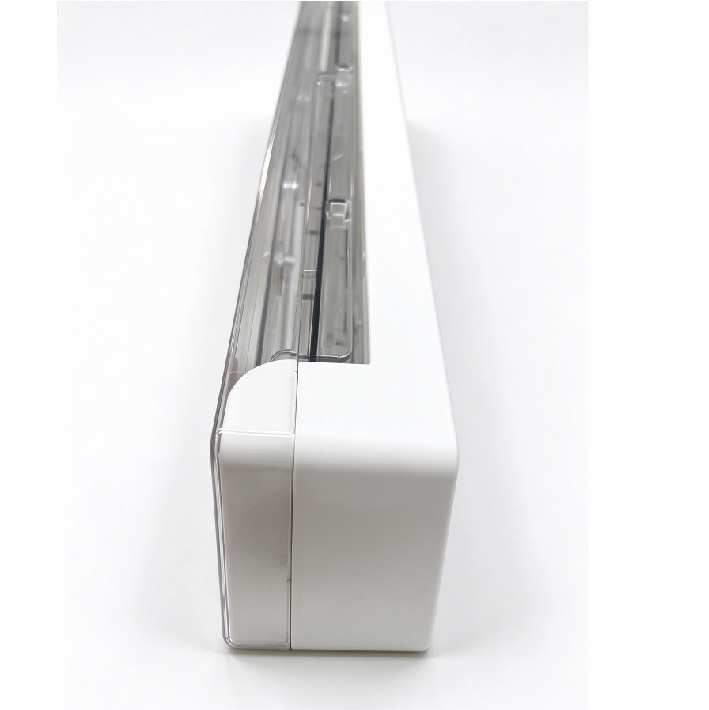
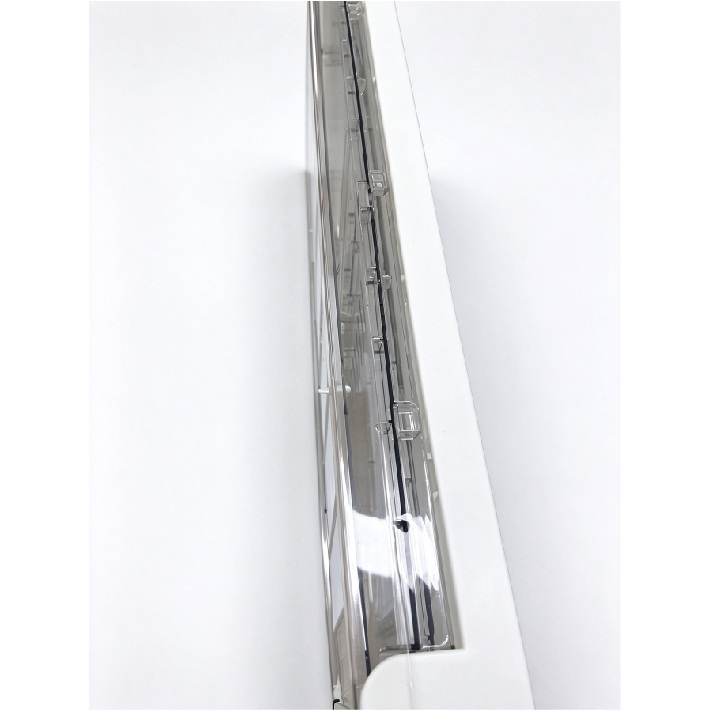
This folding pet enclosure base features a modular construction. All four side walls are removable from the base. The internal depth of the base is purposefully sized to accommodate inward folding of the four panels, optimizing the package footprint to the smallest possible size. Once folded, the side panels nest inside the base and sit closely against one another with little clearance. This structure significantly absorbs shocks during shipping and delivers superior protection for the whole enclosure.

Clarity is a mold decision before it is a resin decision

Clarity is a mold decision before it is a resin decision

A clear wall only looks clear if the light passes through it without scattering, and that is decided in the cavity. The S136 insert is polished in one direction and finished by hand around the corners, where a machine cannot reach without leaving a swirl.
The gate sits where a flow mark will land on a hidden edge instead of on the face, and the PET is dried hard before the shot - moisture in PET is what turns a clear wall hazy, and no amount of polishing fixes it afterwards.
Haze is checked on a sample from every lot against the first approved part, not just at T1.

How to Maintain Flatness for Extra-Large Collapsible Pet Enclosures

How to Maintain Flatness for Extra-Large Collapsible Pet Enclosures

1. The lid presents as a visually flat panel, which creates the primary technical challenge. For this wide, flat PET component, inconsistent wall thickness will induce sink marks at thickness transition boundaries and edge warpage. Perimeter reinforcing ribs are implemented on the PET part. Combined with well-designed gating and optimized injection process parameters, we achieve acceptable part quality.
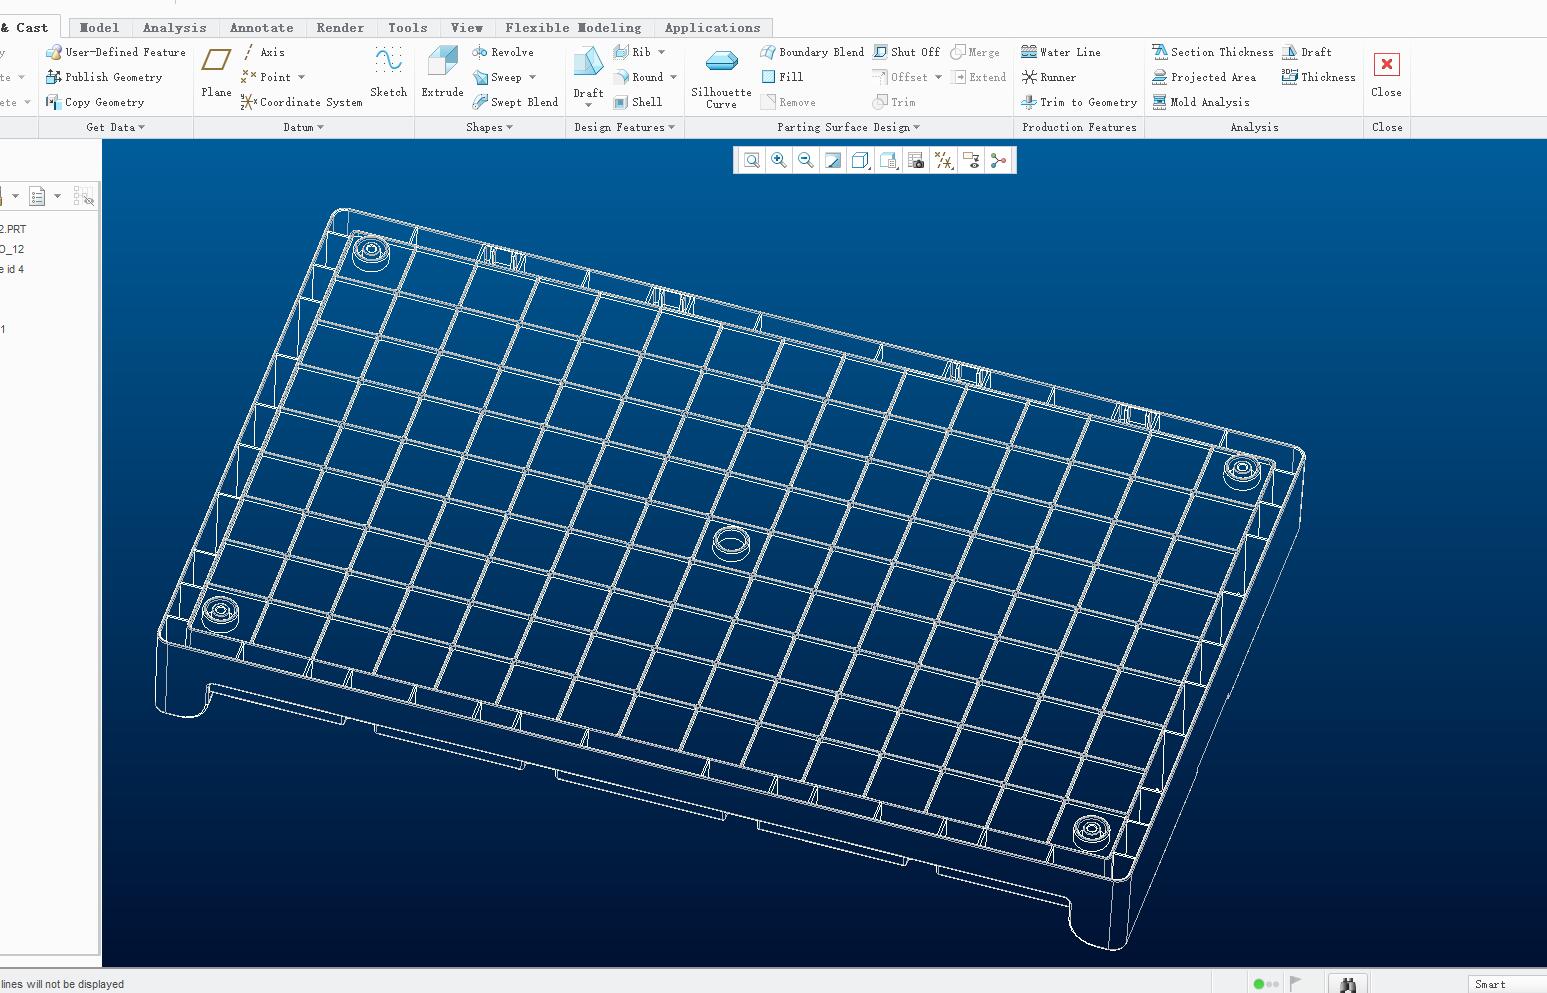
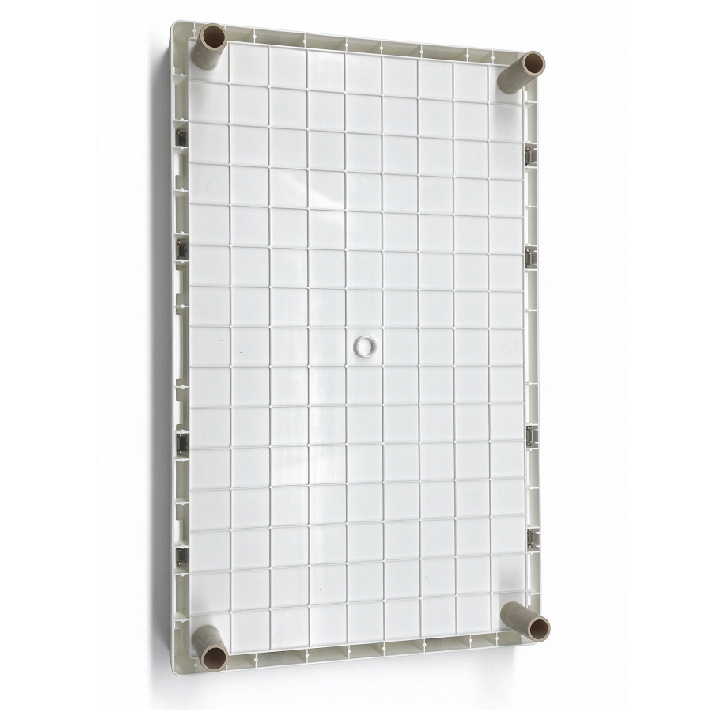
2. The grid-style rib layout on the underside of the ABS base provides structural stiffness. This enables a thin outer surface with consistent wall thickness. Non-uniform wall thickness leads to differential shrinkage and distortion of large panels: thicker regions cool at a slower rate than thin sections and pull the edges downward.
An extra benefit of this grid structure is maintaining sufficient flatness of the base bottom surface. This allows the under-base heating pad to make intimate contact without air trapped in between.

The pet enclosure base and related accessories are plastic parts.

The pet enclosure base and related accessories are plastic parts.

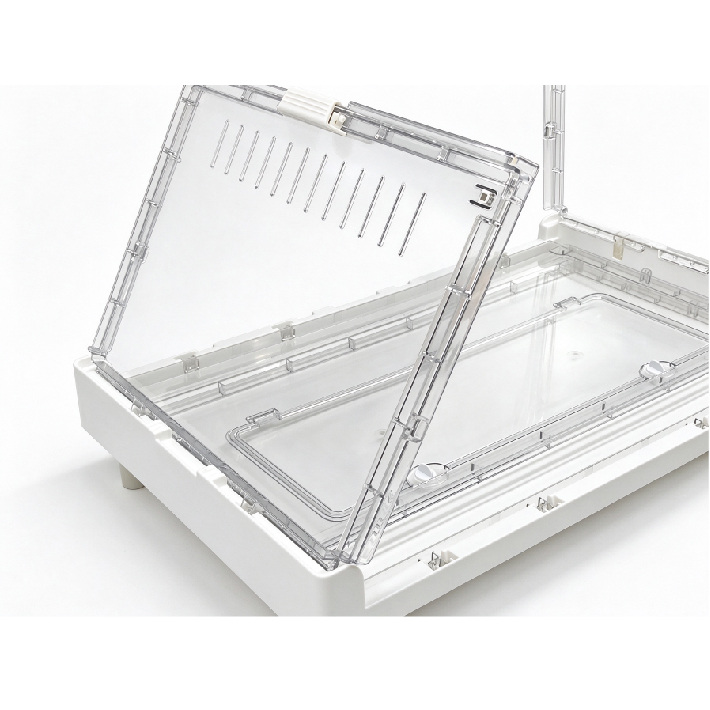
Any metal hardware installed within a humid pet enclosure carries a risk of rust formation in service. This product features an all-plastic construction with no metal parts at all. Its four supporting feet are hollow cylinders integrally molded as part of the base. The lid’s hinging motion is achieved via integrated latch structures on the rear edge, while the two front locking latches are formed as an extension of the enclosure rim.

The design removes the need for separate hardware packs and screwdriver assembly, and eliminates rust-related after-sales complaints. In addition, the lid is captive and cannot be installed upside down. This is highly valuable for retail outlets when delivering units to buyers. The full enclosure can be assembled manually without any extra tools for user-friendly operation.

VERSATILE COMMERCIAL APPLICATIONS

Understand How Pet Product Integrators, Corporate Buyers and R&D Engineers Define Collapsible Enclosures

Reptile and Amphibian Keeping

The transparent enclosure walls enable unobstructed viewing of the inhabitant without opening the access door. This represents a key design priority: opening the lid repeatedly can induce stress in timid small animals. Ventilation channels are integrally formed around the perimeter of the top lid. This structure facilitates cross-airflow and eliminates the requirement for mesh screens that are susceptible to rusting.

Feedback from Pet Product Enterprise Buyers

This pet habitat base supports optional upgraded taller side fences. The taller enclosure panels are custom-designed as an independent part while retaining the same latching interface. They can be assembled onto the existing base and remain compatible with other related components, eliminating the need for new mold tooling.

Key Concerns of Pet Product Integrators

The base designed for reptile enclosures is engineered with stacking capability from the initial design phase. It supports stacking of 3 to 5 enclosures. The base can sit securely on the upper enclosure panel to save space for multi-pet breeding.

Retail and Private Label Kits

Single-cavity mold. The base is available in multiple color options, and custom colors can be developed against customer-provided color chips. The main barrel remains transparent. Logos are printed on ABS components and outer cartons. Additional SKUs can be launched without extra tooling charges.

Design Description of Transparent Panels and Integrally Molded Base

The key to long-term robustness of this housing — staying rigid without deformation, loose joints or rattling noise after years in service — lies in mold steel grade selection, grid-style reinforcing rib arrangement and product design simulation analysis.

Integrally molded structure with no visible seams on the underside

Integrally molded structure with no visible seams on the underside

This bottom housing is integrally molded in one piece with no spliced joints. The large base adopts a large open gate gating scheme. It enables rapid cavity filling and avoids weld lines that would appear on spliced assemblies.

Reinforcing Rib Design Methodology for ODM Pet Enclosure Plastic Base

Reinforcing Rib Design Methodology for ODM Pet Enclosure Plastic Base

For supporting ribs on large molded plastic parts, the standard rib thickness is capped at 0.05 in with a maximum spacing of 2.35 in. These values are adjusted according to actual application scenarios. Reinforcing ribs are laid out uniformly, and their structural adequacy is validated by stress analysis.

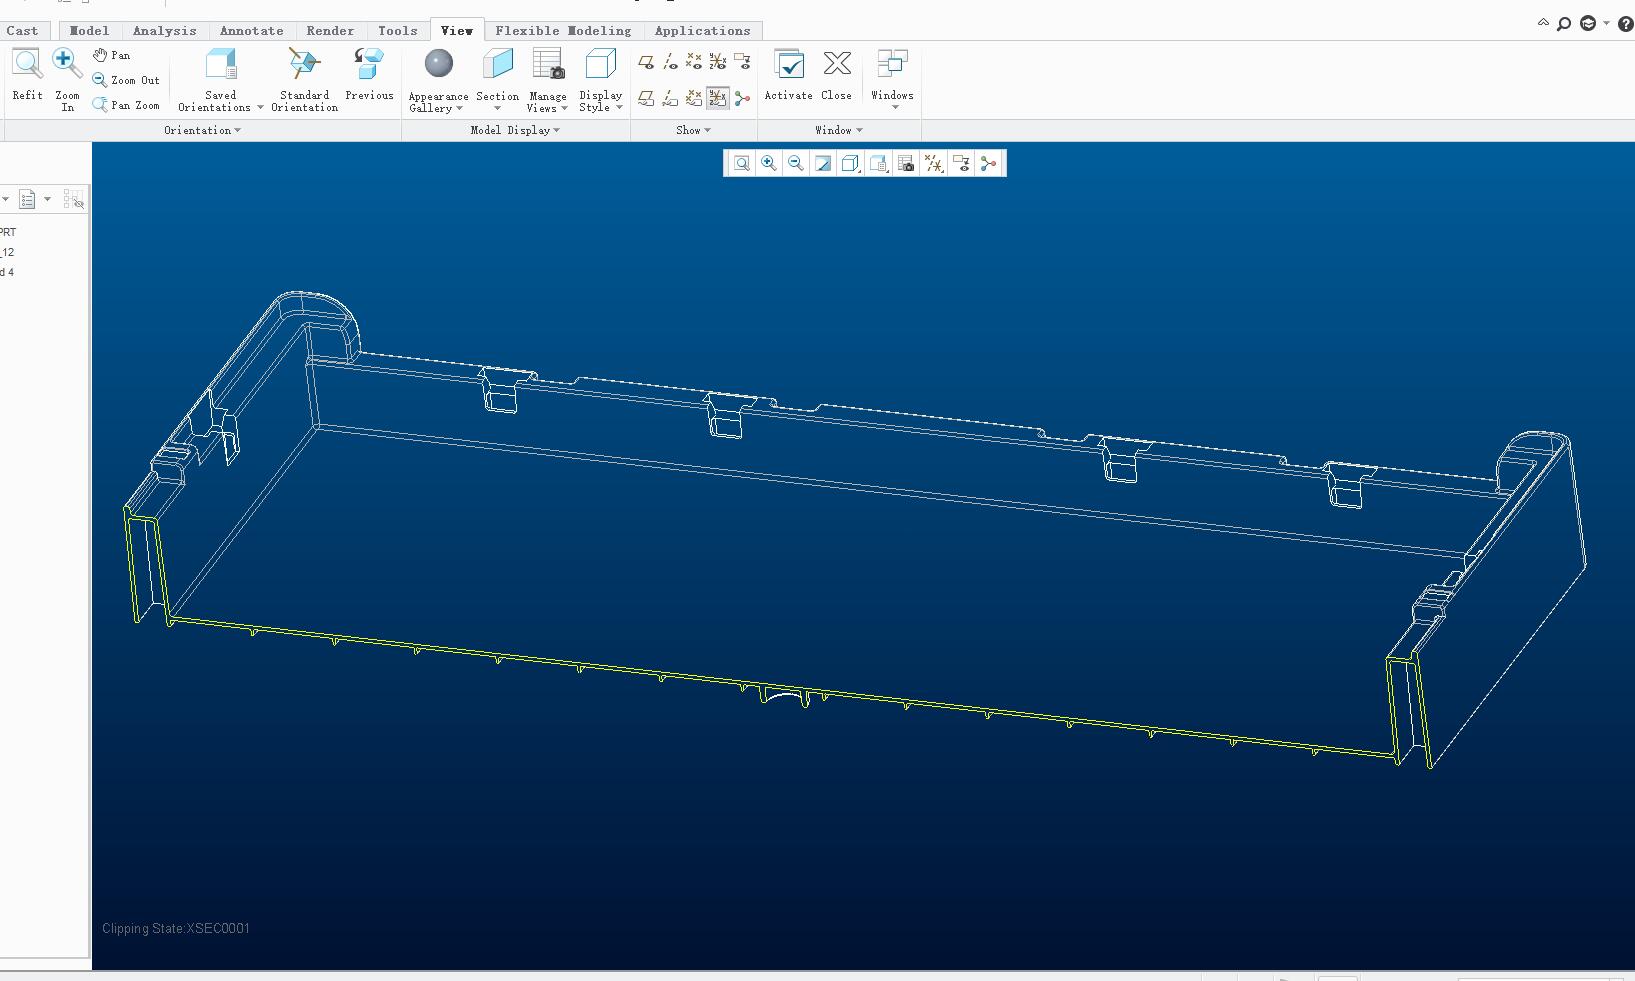
Section Structure Analysis & Inspection of Engineering Drawings

Section Structure Analysis & Inspection of Engineering Drawings

Drawing review for OEM plastic housings of pet enclosures. The specified minimum wall thickness for large-format plastic base shells is 0.1 in. Deep, narrow holes are prohibited on molded parts due to insufficient cooling capacity of the mold cooling circuit. Smooth and consistent wall thickness transitions are required, and generous clearance must be allocated for lifter mechanisms.

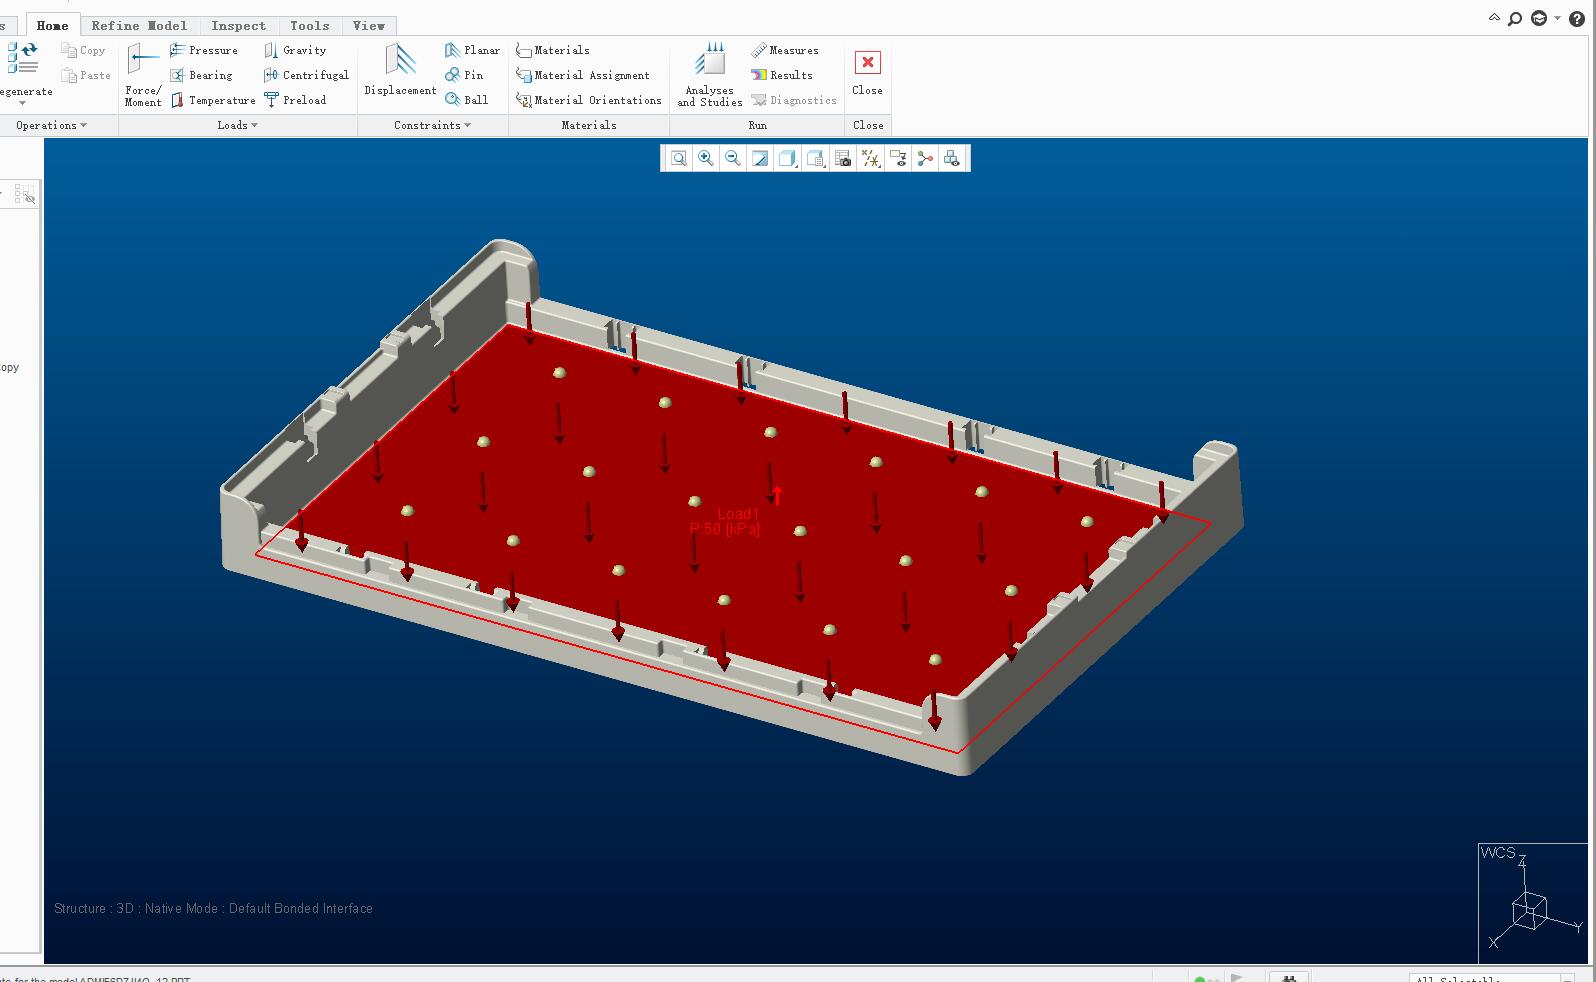
Load-Bearing Stress Analysis for Pet Enclosure Base

Load-Bearing Stress Analysis for Pet Enclosure Base

Since different pet accessories, some with substantial weight, will be placed inside the enclosure, the base must be designed with load-bearing capability in mind. Stress analysis output defines design specifications to guide wall thickness sizing and reinforcing rib arrangement.

Commercial Terms & Certification

الحد الأدنى للطلب OEM/ODM

Custom colour, logo and retail packaging start at 500 sets.

Samples are available from a single unit, machined or from a T1 shot.

مهلة الإنتاج

Tooling and T1 samples (718H plus one S136 insert) 25-30 working days after DFM sign-off

Pilot run and clarity approval 5-7 working days

Mass production, 500 sets 15-18 working days

Sea freight to EU or US 25-35 days

التغليف القياسي

1 set x ABS base, nested under the tub

10 sets x Export carton, lids kept flat to protect the clear wall

Spare lids packed flat in their own carton if ordered

Custom retail carton quoted separately

Prices are quoted against a confirmed drawing, resin grade and quantity. Tooling is charged once and stays in production for repeat orders.

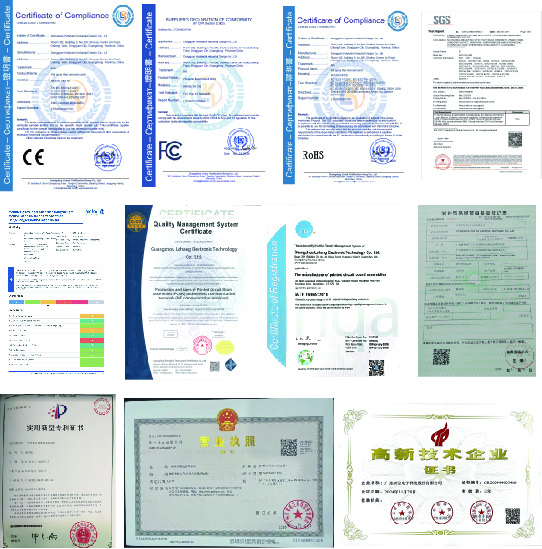
Certification Support

We prepare the material and test documents for the certifications below and run pre-shipment checks against them, so your own compliance file is complete before the container leaves.

RoHS REACH SVHC ISO 9001 FDA GPSR EN71 UKCA

Looking for Customization or Bulk Orders?

From individual CNC-machined samples up to bulk stacked pet enclosure packs, we offer full one-stop manufacturing covering plastic parts and outer carton packaging.

Packaging Scheme Specification for Collapsible Pet Enclosure

1. Each individual base shell is enclosed in a bubble bag together with foam cushion inserts and placed inside a 5-ply carton. Five assembled sets are bundled and loaded into one outer master carton.
2. We conduct simulated drop tests and full truck load road simulation over a 50-kilometer route to replicate real transportation conditions for validation.

Why the tub is PET and the base is ABS

Reptile enclosures have two conflicting requirements for a single unit. The side walls need high transparency for viewing animals without opening the lid, while the base must have sufficient rigidity to sit steadily on floors or shelves and support the full weight when the enclosure is lifted.

PET meets the first requirement. It is the same resin family used for clear beverage bottles. With properly selected wall thickness, it delivers light transmission without light scattering.

ABS satisfies the second requirement. It can be molded with reinforcing rib grids and integrated support feet, and supports custom color matching to expand brand SKUs.

These two materials require different mold steels. PET is hygroscopic, with high melt temperature and moderate flowability. It needs highly polishable cavities whose polished surface can withstand cleaning between injection cycles. Carbon steel cavities polished for ABS will show machining marks through the transparent PET walls after a few thousand shots.

ABS can be stably molded on pre-hardened 718H mold steel. This grade is more cost-effective, offers better crack resistance for deep ribs, and delivers a matte finish directly after texturing. We use separate mold steels for this project. Although tooling cost is slightly higher at the mold stage, it ensures consistent quality from prototype to mass production.

Successful Case Introduction: Clear Reptile Tub on a Molded Base

Case A - Clear enclosure for a reptile and amphibian range
Part: PET tub and lid, ABS base with four molded feet and a ribbed lid panel
Material: PET, optical clarity (tub, lid); ABS, impact-modified (base, lid frame)
Size: 27.6 x 16.9 x 3.0 in overall
Mold: ABS parts in 718H pre-hardened steel, 30-34 HRC, matte texture; PET cavity in S136 stainless, polished to SPI A-2

What the project needed: the buyer was already buying this footprint from a molder who could not hold the clarity past the third shipment, and wanted the lid to stop arriving with loose hinge pins. The brief was to keep the rack footprint, drop the hardware and make the wall read clear on a retail shelf.

Result: the hinge became two molded barrels, the catches became part of the rim, and haze is now checked per lot against the approved sample rather than per shipment.

Technical Specifications

الخامة

side pane: PET, optical clarity | Base and lid frame: ABS, impact-modified

الحجم الكلي

27.6 x 16.9 x 3.0 in

Process

Injection molding; PET parts single-cavity, ABS parts single-cavity per part

Mold steel

ABS parts: 718H pre-hardened, 30-34 HRC | PET cavity: S136 stainless

Cavity finish

PET: polished SPI A-2 | ABS: matte texture, SPI C-1

Nominal wall

0.10 in tub and lid / 0.09 in base and frame

Draft angle

1.0 deg on the side walls, 1.5 deg through the rib grid

Latching

Two molded turn catches at the rim, lid on molded hinge barrels

Stacking

Four hollow feet locate into the rim of the tub below; stack height held across sizes

التغليف

1 set per PE bag, 10 sets per export carton, lids kept flat

From Footprint Drawing to Latched Enclosure

الخطوة 1 Requirement and DFM - send the footprint, the stack height you already use, the vent area, the divider positions and the resin you want on the base. We return a DFM report with wall, rib, draft and gate positions, plus the two steel choices. Send Requirements
الخطوة 2 Mold Making and T1 Samples - 718H cavities for the ABS parts, an S136 insert for the PET cavity polished to SPI A-2, T1 shots in both resins, tub and base trial-assembled on the bench.
الخطوة 3 Pilot Run and Clarity Approval - 50 to 100 sets on the released tools. Haze, colour, latch effort and stack height are signed off against a retained sample before the batch is released.
الخطوة 4 Mass Production - 500 sets and up. Clarity and colour checked against the approved sample every shift, flatness checked on a surface plate, dimensional report per lot.
الخطوة 5 Packaging & Shipment: Side panels are nested together. Lids are laid flat without touching the enclosure walls. Foam separators are placed between each part. Ten sets are packed per export carton. Retail color boxes are produced according to your artwork.

الوثائق والموارد الفنية

Why do the two parts need different mold steels?

Because they are two different resins doing two different jobs. The ABS parts - base, lid frame - run in 718H, a pre-hardened chromium-molybdenum steel at about 30-34 HRC: it takes a deep rib and a matte texture without the distortion a through-hardened block risks. The PET tub and lid run in S136 stainless, which resists pitting from a hygroscopic resin and can be polished to SPI A-2 and re-polished after a tool service. A carbon-steel cavity polished for ABS will start to show its tool marks through a clear wall within a few thousand shots.

How do you keep the PET wall optically clear?

Four things, in this order: the resin is dried hard before the shot, because moisture in PET is what turns a clear wall hazy; the gate is placed so the flow mark lands on a hidden edge; the cavity is polished in one direction and hand-finished where the corners are, because a clear part shows every polishing swirl; and the wall is kept uniform, so the light does not bend at a thick-to-thin transition. Haze is measured on a sample from every lot against the approved part.

Why is the base ribbed instead of a solid panel?

For a flat wall measuring 0.09 in thick and 27.6 in wide, sink marks tend to form between raised bosses, together with edge warpage as it cools. Grid reinforcing ribs deliver structural rigidity, which enables a thin outer surface with uniform wall thickness — and uniform wall thickness is critical to maintain part flatness.

Will the clear wall yellow under a heat lamp?

End users place heating devices on the top mesh for electric heating. As a result, the enclosure is exposed to warm air instead of a hot surface. If the enclosure will be located under basking lamps or UV-fitted racks, please inform us at quotation. We will use UV-stabilized PET resin to replace the standard grade. This change is only noted on the resin datasheet and requires no mold modifications.

Can the vents, divider slots and lid depth be changed?

Yes - all three are cut into the tool, so position, count and depth are part of the tool design and cost nothing extra to agree before the cavity is cut. Send the vent area you need and the divider positions. If the vent pattern is likely to change again, the vented area can be run as an interchangeable insert so the main cavity is not re-cut.

FREQUENTLY ASKED QUESTIONS - REPTILE ENCLOSURES

What is the minimum order, and what does the first order include?

MOQ for custom colors, user manuals, logos and retail packaging is 500 sets. The initial order generally includes tooling, T1 samples, 50–100 pilot-run units, plus transparency and dimensional inspection reports. Samples produced before this phase are standalone CNC-machined prototypes.

How is the enclosure priced - per set or per part?

The quote is per set, built from the shot weight of each of the four parts, the cycle time on each tool and the packing you ask for. We show the PET and the ABS weights separately, so you can see what the clear wall contributes.

ما الملفات المطلوبة لعرض السعر؟

Kindly submit 2D engineering drawings or 3D CAD files in STEP / IGES format for the main enclosure body, lids and base shell, together with color reference samples, required order volume and full test specifications. For new development projects, please also provide the product specification document and the reptile/small animal species this habitat is designed for.

كيف تحمون تصميمنا وقوالبنا؟

An NDA is signed before drawings change hands. Tooling paid for by you is booked under your name and can be moved out on written request; we do not quote the same custom footprint to another buyer.

What is the lead time for a repeat order?

Reorder production lead time for 500 sets of plastic base shells is 10 working days, excluding ocean shipping transit time. If new color matching is required for ABS resin, an additional 5 working days are needed for masterbatch preparation and color chip sampling.

لماذا تختارنا

Top Tier OEM/ODM 20+ Years | Custom Large Smart Pet Products

أكثر من مليون
Annual Capacity
30+
R&D Team
ODM/OEM
20+ Years
الشهادات
CE/FCC/RoHS/FDA/IEC62368

الشهادات الدولية

نحن شركة عالية التقنية تجمع البحث والتطوير والإنتاج والمبيعات، ولدينا فريق متخصص في التصميم الصناعي والإلكتروني والإنشائي. حاصلون على ISO9001 وBSCI ونخدم أكثر من 200 عميل حول العالم.

الشهادات الدولية
FCC
CE
CE-EMC
REACH
RoHS
UN38.3
IEC62368
FDA
FCM
GPSD
UL/ETL IEC62368-1
FCM EU 10/2011
UL94

اتصل بنا نحن

يسعدنا التواصل معك!

العودة إلى جميع الخدمات